Scrap Reduction in Manufacturing: 7 Techniques That Actually Work
Seven scrap reduction techniques for manufacturing plants, plus a plain formula for the true cost of scrap and a way to decide which line to fix first.
- Scrap you can't tie to a cause can't be fixed. Record defect type, line, shift, part and time for every scrap event.
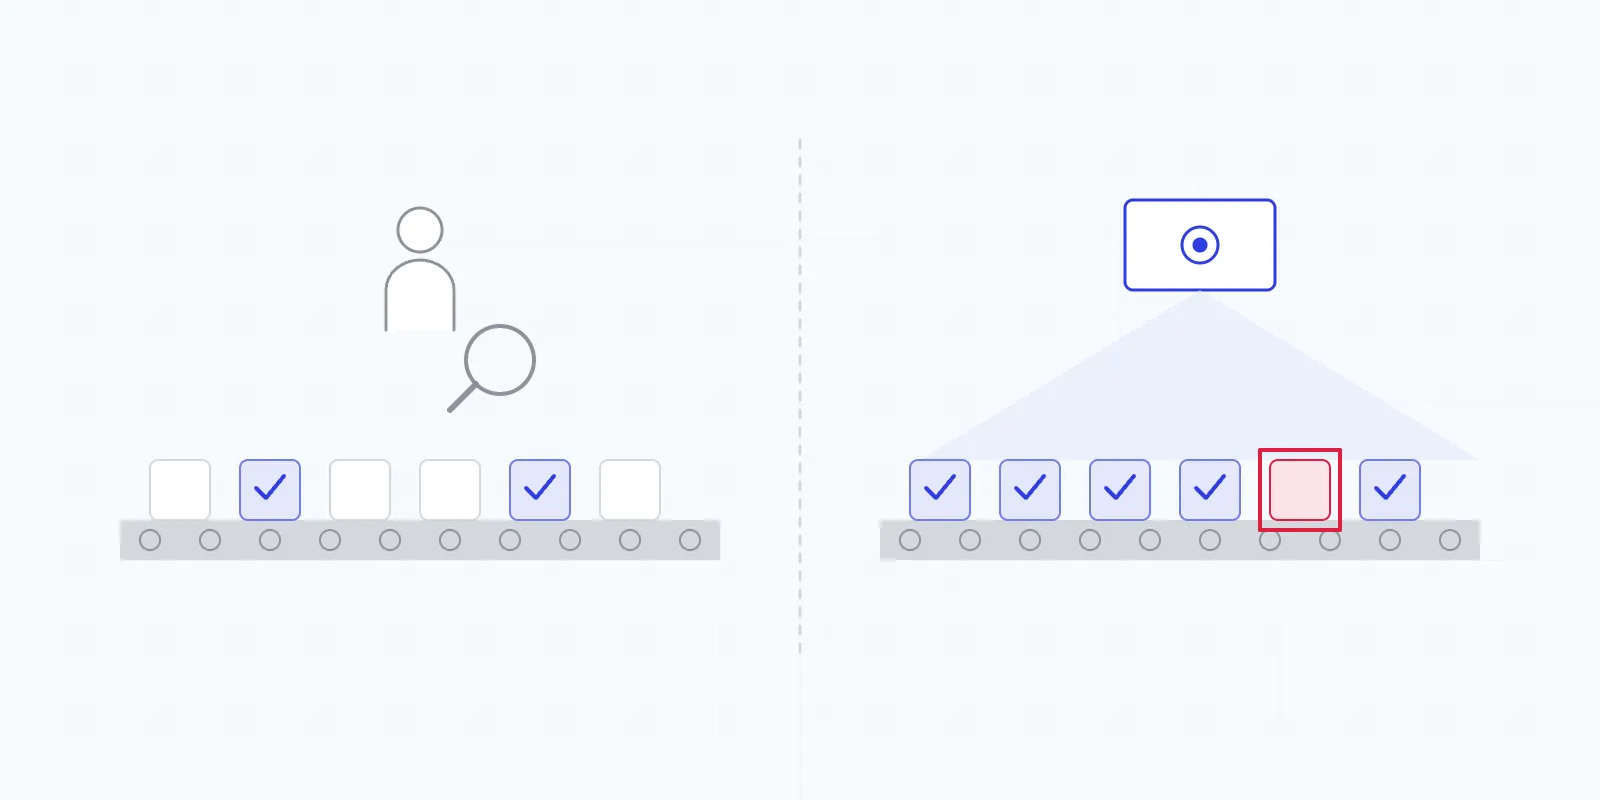
- The earlier a defect is seen, the less it costs. Catching a problem at the source in seconds turns a lost roll or bin into a handful of parts.
- Detection pays off when it drives action: rejects, alerts and process corrections wired into the line, plus roll and lot traceability so only the bad material is scrapped.
- Start with the 5–10 part and defect combinations that cost the most, and expand once they're under control.
Most plants already know their biggest scrap drivers. What stops scrap reduction in manufacturing is usually the data: scrap gets measured too late and too coarsely to act on. It turns up as one percentage in a monthly report, long after the shift that made it has gone home.
There are two ways to cut scrap, and plants tend to chase only one. You can make fewer bad parts, or you can throw away less good material along with the bad. Scrapping a whole roll for one defect, or a whole bin for one bad part, is often a bigger loss than the defect itself, and several of the techniques below deal with that second kind.
They’re listed roughly in the order we’d apply them. Before any of them, it helps to put a dollar figure on the problem.
Pricing a scrapped part
Scrap costs more than the material in the bin. By the time a part is thrown away, you’ve paid for its material, the labor and machine time to make it and a share of overhead, and sometimes a lot more than that downstream.
Run the formula per line, per shift and per part and defect combination, with your own inputs. The ranking matters more than the total. It’ll usually show that a small group of combinations accounts for most of the cost, and those are where you start.
The techniques
-
Measure scrap by cause, line and shift. One plant-wide percentage can’t tell you what to fix. Record every scrap event with defect type, line, shift, part number and time, and patterns appear: one tool, one shift change, one resin lot, one operator habit. Each of those needs a different fix. Manual scrap tags work when people fill them in every time, and cause codes are the first thing to get skipped on a busy night shift. Automated inspection writes the cause with every detection, so the record is complete without anyone thinking about it.
-
Catch defects where they’re made. A defect gets more expensive every minute nobody sees it. Found in seconds, a problem costs a few parts. Found at the next roll change, bin audit or customer dock, it costs a truckload. At a steel stamping plant, AI inspection flagged a defect spike on a night shift within 10 seconds, which prevented more than 10,000 defective parts. That catch happened because the camera sat at the process instead of at final inspection. What is AI visual inspection explains how inline systems are built.
-
Wire detection to action. Rejecting a bad part is containment. Stopping the next one is prevention, and it takes a connection between the camera and the line. PLC signals fire reject gates, kick-offs, robots and flaggers so bad parts leave the flow without anyone chasing them. Process corrections, made as soon as a defect trend shows up, fix the cause. Audible alerts get an operator to the press or the die while the problem is small. Injection molding defects shows what that loop looks like at a molding press.
-
Hold every shift and plant to one standard. If day shift rejects a mark that night shift accepts, your scrap rate partly measures who’s working. People see differently, and they get tired. One inspection standard applied the same way on every line removes that variation, and it makes scrap rates between plants comparable. For a multi-plant operation that’s a big change. Until the standard is shared, a plant with a low scrap rate might simply be one that accepts more, and nobody can tell the difference from a report.
-
Track leading indicators alongside the scrap rate. Scrap rate is a lagging number. SPC on key dimensions and defect counts shows drift before parts go out of tolerance. Cpk tells you whether a process can hold its spec at all. First-pass yield includes the rework and re-inspection that the scrap rate hides. Feed those charts with inspection data from every part instead of a sample, and they get far more trustworthy.
-
Rank root causes from defect trends. Once every defect carries a type, time and location, clusters show up. Scratches line up with one idler roll. Gas burns gather on one cavity after the vents start to clog. Holes go missing right after a die change. Rank those causes by cost, fix the top one, and check that its trend line actually drops before moving on.
-
Scrap only the bad section. On film and coil, the default response to a known defect is often to scrap or downgrade the full roll. A roll map records where every defect sits, so the slitter can cut out the affected section and keep the rest. On discrete parts, lot traceability shrinks a quarantine from a week’s production to one lot and one time window. A flexible packaging producer running inline inspection with roll reports on four film lines cut scrap by 25% and customer claims by 50%. The details are in AI defect detection for plastic film.
Who needs to see the savings
The same scrap data has to answer different questions depending on who asks.
| Role | The question | What to show |
|---|---|---|
| Plant manager | What’s this worth on my floor? | Scrap rate and dollars recovered per shift and per month, by line |
| VP / Director of Operations | Is it working across every plant? | A rollup of scrap rate and dollars, standardized so plants compare |
| Quality leader | Are we shipping fewer defects? | Customer claims, escapes and audit evidence |
| Process engineer | What should I fix next? | Defect trends by cause, Cpk on key dimensions and first-pass yield |
A plant manager acts on dollars per shift on a named line, because that’s something they can take to the morning meeting. A VP of operations wants to see the same technique, applied the same way, bringing scrap down at every site. Quality wants to know escapes are falling, and the process engineer wants the next thing to fix. Tristar’s dashboard is built around the first two rows: line detail for the plant, and a cross-plant rollup for leadership.
Picking where to start
Don’t try to cover every SKU in a high-mix plant at once. Take the cost-of-scrap ranking from the formula above and pick the 5–10 part and defect combinations at the top. They usually carry most of the cost, and a short list gives you a clean before-and-after comparison.
When choosing between two candidates with similar cost, pick the one where the defect is visible and the cause is fixable at the line. A burn on a seal jaw or a missing hole from a broken punch will show results quickly, because a camera can see it and an operator can act on it. A defect that only appears in a lab test or at the customer is a harder first project.
Then check what the line can do with a detection. If there’s already a reject gate, a PLC you can signal and someone on shift who can adjust the process, that line is ready. If not, add the integration to the plan before the cameras. Once the first combinations are under control, expand line by line, and use the evaluation checklist when you bring vendors in.
Frequently asked questions
What is scrap reduction?
Scrap reduction is lowering the amount of material and product thrown away or downgraded because it fails quality requirements. It covers preventing defects and also limiting how much good material gets scrapped along with the bad.
How do you calculate the cost of scrap?
Multiply scrapped units by the full cost already put into each unit (material, labor, machine time and overhead), add disposal and downstream costs such as re-inspection, rework and claims, and subtract any salvage or regrind value.
What is a good scrap rate?
It depends so much on process, material and product mix that an industry-wide figure isn't very useful. Compare each line against its own baseline and against your best line or shift running the same parts.
What does scrap reduction software do?
It records where, when and why scrap happens. Tools range from manual scrap logging in MES to AI visual inspection that checks every part in real time, alerts operators and ties each defect to a line, shift and lot.

Our engineers design and deploy AI inspection systems on plastic film, injection molding, metal stamping and automotive assembly lines across North America.